
Hot work tool steel with good hot properties and an excellent thermal conductivity for hot work applications with intensive cooling
2365 PRIME;
- is a 3% chromium and 2.8% molybdenum hot-work tool steel produced by a process that ensures a good level of cleanliness
- has a good hot strength and tempering back resistance.
- has an excellent thermal conductivity and is suitable for hot work tools cooled by water.
- can also be welded and exhibits good machinability.
- has a very good suitability for surface treatments such as gas, ionic or salt bath nitriding, as well as PVD or CVD coatings.
Applications
2365 PRIME is suitable for the manufacture of die inserts and forging machine tools, die casting molds of light and heavy alloys, as well as spindles, mandrels and spinning punches.
Compared to CUDA PRIME steel (1.2343), 2365 PRIME has a better thermal conductivity and is suitable for hot work tools intensively cooled (by water for example).
Main properties
- Excellent thermal conductivity
- Suitable for hot work tools cooled by water
- Good hot strength and tempering back resistance
- Suitable for surface treatments
Chemical composition (typical)
| C | Mn | Si | P | S | Cr | Mo | V |
|---|---|---|---|---|---|---|---|
| 0.32 | 0.30 | 0.30 | ≤ 0.025 | ≤ 0.025 | 3.00 | 2.80 | 0.50 |
Designation
| Werkstoff Nr | ISO | China GB | JIS Japan | UK | AISI USA | Russia Gost | AFNOR | Other / Special |
|---|---|---|---|---|---|---|---|---|
| 1.2365 | 32 CrMoV 12 28 | 4Cr3Mo3SiV | SKD7 | BH10 | H10 | – | Z32DCV28 | – |
Structure
The structure of the 2365 PRIME is fine and homogeneous without precipitation or alignments of carbides.
Hardness at the time of delivery
Annealed for 230 HB max.
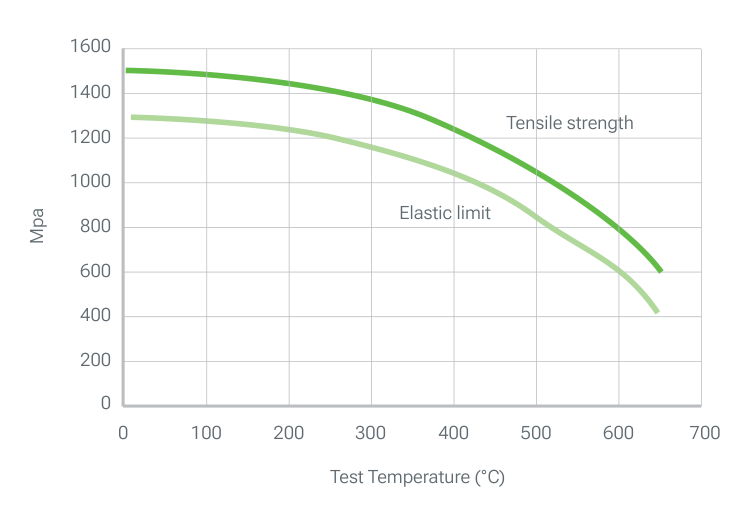
Typical mechanical properties in hardened conditions at different temperatures (results from internal tests not indicated on the certificates)
Physical properties
| Temperature | 20°C | 200°C | 400°C | 600°C |
|---|---|---|---|---|
| Volumic mass kg/m3 | 7800 | 7770 | 7700 | 7540 |
| Young Modulus N/mm² | 205000 | 198000 | 177000 | 130000 |
| Thermal conductivity W/m.K | 32 | 31.9 | 32.5 | 30 |
| Coefficient of linear expansion 10-6/K | 12 | 12.5 | 13.1 | 13.5 |
Heat treatment
Soft annealing
Temperature: 730 – 770°C, duration 1h + 1h for 25 mm thickness. slow cooling in the furnace (10 to 20°C/h). The atmosphere in the furnace must be reducing to avoid decarburization of the steel.
Stress relieving
After machining, it is recommended to perform stress relieving for a minimum of 2 hours, followed by slow cooling in the furnace to 450°C.
Austenitization
In order to avoid any risk of cracking it is recommended to preheat in 2 steps.
- 1st preheating step: temperature: 550°C time: 30 s/mm of thickness
- 2nd preheating step: temperature: 750°C time: 30 s/mm of thickness
Recommended austenitizing temperature: 1010 – 1030°C. The holding time should not be too long to avoid a risk of grain coarsening and a loss of toughness. It is recommended to keep the part at the austenitizing temperature 30 minutes per inch of thickness as soon as the temperature of the surface reach the austenitization temperature.
Quenching medium
Oil at 80°C, vacuum (pressure > 6 bars), salt bath 500 – 550°C.
To ensure good toughness, treatment with oil or salt bath is preferable.
Tempering
To ensure a minimum residual austenite rate as well as greater tool stability, it is essential to perform a double tempering. It is recommended to perform the first tempering at a temperature of 500°C to ensure optimal carbide precipitation. The second tempering will be carried out at an appropriate temperature depending on the desired hardness. Each tempering is followed by a cooling under 100°C.
Each tempering time must be at least equal to 1h + 1h for 25 mm of thickness of the treated part (equivalent thermal thickness).

Surface treatment
Nitriding
2365 PRIME can be nitrided at temperatures less than or equal to 20°C below tempering temperatures without risk of deterioration of the mechanical characteristics.
PVD, CVD
2365 PRIME is suitable for all kinds of PVD and CVD treatment as soon as the treatment temperature is 30°C lower than the last tempering temperature.
Polishing
2365 PRIME is perfectly suitable for polishing in the treated state and can be used for applications requiring a sufficient level of polish for translucent – transparent parts (Rt ≤ 20 μm, CNOMO level 2, Rugotest N7).
Optimal polishing is achieved by performing consecutive steps with similar roughness and stopping each step as soon as the last scratch from the previous step disappears.
Texturing
2365 PRIME is suitable for chemical or laser texturing.
Machining
The machining parameters below are given for information only and must be adapted according to the equipment and usual machining conditions.
Turning
| Carbide tool Rough machining |
Carbide tool Finishing |
HSS tool Finishing |
|
|---|---|---|---|
| Cutting speed m/min | 140 – 180 | 180 – 230 | 17 – 22 |
| Feed mm/r | 0.2 – 0.4 | 0.1 – 0.2 | 0.1 – 0.3 |
| Depth of cut mm | 2 – 4 | 0.5 – 2 | 0.5 – 2 |
Milling: surfacing
| Milling with carbide tools Rough machining |
Milling with carbide tools ½ Finishing |
Solid tool Finishing |
|
|---|---|---|---|
| Cutting speed m/min | 160 – 180 | 180 – 200 | 210 – 280 |
| Feed mm/r | 0.45 | 0.4 – 0.25 | 0.15 – 0.05 |
| Depth of cut mm | 1 – 3 | 1 – 2 | 1 – 0.5 |
Drilling: carbide drill
| Carbide type | Indexable insert | Solid carbide | Carbide tip |
|---|---|---|---|
| Cutting speed m/min | 160 – 180 | 100 – 130 | 55 – 80 |
| Feed mm/t | 0.05 – 0.10 | 0.10 – 0.25 | 0.15 – 0.25 |
Drilling: HSS twist drill
| Drill diameter mm | Cutting speed m/min | Feed mm/t |
|---|---|---|
| < 5 | 14 – 16 | 0.05 – 0.15 |
| 5 – 10 | 14 – 16 | 0.15 – 0.20 |
| 10 – 15 | 14 – 16 | 0.20 – 0.25 |
| 15 – 20 | 14 – 16 | 0.25 – 0.30 |
Fine grinding
General indications for grinding wheels to be used on 2365 PRIME in the heat treated condition
Usually, rather soft vitrified aluminum oxide grinding wheels (grades G for plane grinding to K for cylindrical grinding) are used.
Particular attention will be paid to effective cooling of the surface during grinding to prevent degradation of the material surface.
Electro-discharge machining
2365 PRIME is also suitable for EDM machining (wire or electrode). Preferably, the machining will be carried out with a low current density and a high frequency in order to limit the thickness of the white layer as much as possible.
Then it is necessary to carry out a stress relieving at 25°C below the last tempering in order to reduce the level of residual stresses (which could lead to a risk of cracking) and to carry out a polishing to completely remove the white layer formed during the discharge machining process.
Welding
It is not recommended to weld 2365 PRIME but if this is mandatory it could be welded either in the annealed condition (better) or in the heat treated condition.
- Method: TIG (pure Ar protection)
- Feeder wire: AISI H10
- Preheating: 350°C.
Hold at 200°C during the welding operation with a maximum interpass temperature at 480°C. Slow cooling (max 20°C/h) after welding. - Post treatment:
- In the treated state: tempering at 20°C with a tempering time at least equal to 1h + 1h for 25 mm of thickness of the treated part (equivalent thermal thickness).
- In the annealed state: carry out a soft annealing under the usual conditions: temperature: 840 – 870°C, duration 1h + 1h for 25 mm of thickness. slow cooling in the furnace (10 to 20°C/h).
Download the 2365 PRIME datasheet (PDF)
More grades: Hot Work Tool Steels. Where to buy: Service Network.
