
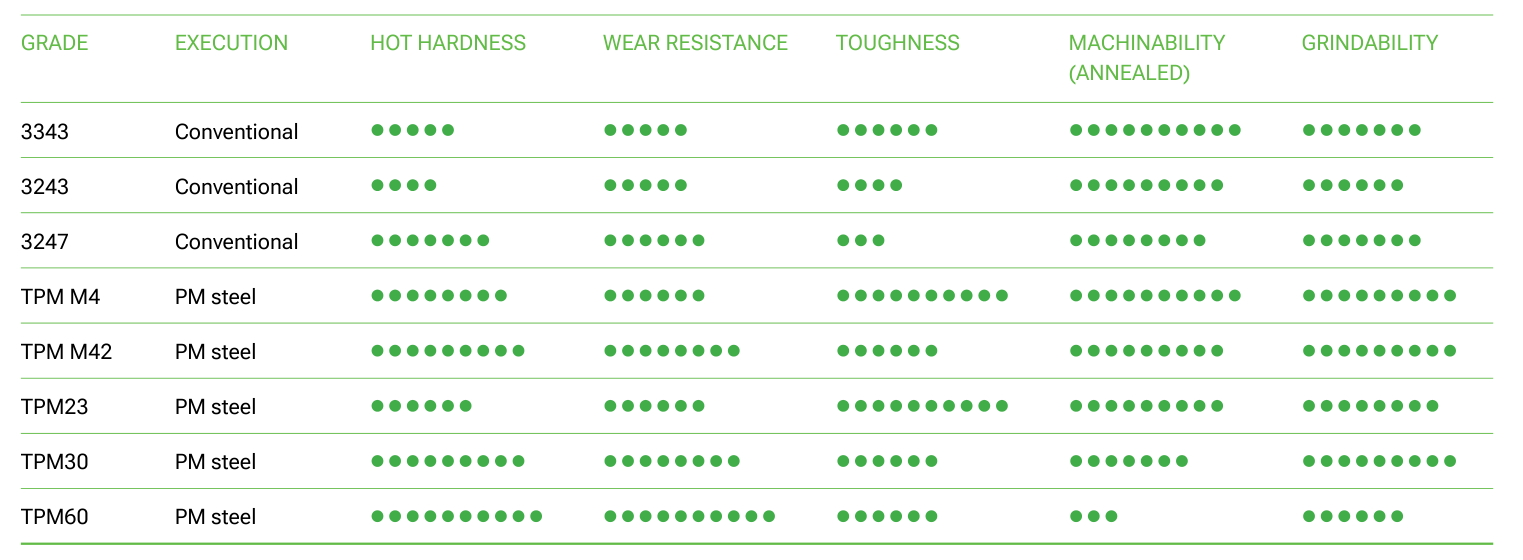
Grain refined High Speed Steel with high wear resistance associated with good toughness
3243 H PRIME;
- is a grain refined high-speed steel that allows it to obtain a very high cleanliness and a very fine structure, which improves its toughness.
- has a high cobalt content and it gives it a high hot hardness as well as a very high resistance to embrittlement on tempering.
- has a very high wear resistance associated with a high hardness and a good toughness.
- shows a good suitability for surface treatments such as gas, ionic or salt bath nitriding, as well as PVD or CVD coatings.
Applications
3243 H PRIME can be used for complex cutting tools with a working area at the surface such as hobs, gear cutters, taps and so on. Thanks to the smaller carbide size, “tips” do not easily break and the hardness is still high and associated with a high toughness.
3243 H can also be used for milling cutters, taps, dies, spindles, reamers, thread rolling combs, segments for circular saws, etc and also, shear blades, cold working cylinders.
3243 H PRIME can be used for fine cutting tools (punches and dies), cold or semi-hot forming tools.
3243 H PRIME can also be used for all tools with very high and cyclic thermal loads.
3243 H PRIME can be used for cavities and injection sills of plastic molds and in some cases for hot work tools due to its high hot hardness.
3243 H PRIME is also used for all kind of parts in contact with highly abrasive materials as porcelain.
Main properties
- Excellent wear resistance
- High resistance to tempering embrittlement
- High hot hardness
- High compressive strength
- High hardenability
Chemical composition (typical)
| C | Mn | Si | P | S | Cr | Mo | V | W | Co |
|---|---|---|---|---|---|---|---|---|---|
| 0.88 | 0.34 | 0,35 | ≤ 0.030 | ≤ 0.003 | 4.05 | 5.02 | 1.81 | 6.05 | 4.58 |
Designation
| Werkstoff Nr | ISO | China GB | JIS Japan | UK | AISI USA | Russia Gost | AFNOR | Other / Special |
|---|---|---|---|---|---|---|---|---|
| 1.3243H | HS 6 5 2 5 / X90WMoCoCrV 6-5-5-4-2 | W6Mo5Cr4V2Co5 | SKH55 | BM35 | M35 | P6M5K5 | – | – |
Comparison HSS grades
Structure
The structure of the 3243 H PRIME is fine and homogeneous without precipitation or alignments of big carbides. The carbide distribution and the micro cleanliness are controlled and in conformity with the Stahl-Eisen Werkstoff Blatt 1570 / 61 standard.
The austenite grain size is determined on the surface of the specimen according to Snyder-Graff method. The minimum permissible values (average of 10 measurements) before tempering are given below.
| Section (mm) | Austenitic grain size |
|---|---|
| 0 – 25 | 12 |
| 25 – 50 | 11 |
| 50 – 125 | 10 |
| > 125 | 9 |
Hardness at the time of delivery
Annealed for 300 HB max.
Physical properties
| Temperature | 20°C | 350°C | 700°C |
|---|---|---|---|
| Volumic mass kg/m³ | 8120 | 7930 | 7725 |
| Young Modulus N/mm² | 217000 | 198000 | 175000 |
| Thermal conductivity W/m.K | 20 | 18.7 | 18.0 |
| Coefficient of linear expansion 10-6/K | 9.8 | 11.2 | 12.6 |
Heat treatment
Soft annealing
Temperature: 820 – 880°C, duration 1h + 1h for 25 mm thickness. slow cooling in the furnace (10 to 20°C/h). The atmosphere in the furnace must be reducing to avoid decarburization of the steel.
Stress relieving
After machining, it is recommended to perform stress relieving at 600 – 650°C for a minimum of 2 hours, followed by slow cooling in the furnace to 450°C.
Austenitization
In order to avoid any risk of cracking it is recommended to preheat in 3 steps.
- 1st preheating step: temperature: 500°C time: 30 s/mm of thickness
- 2nd preheating step: temperature: 850°C time: 30 s/mm of thickness
- 3rd preheating step: temperature: 1050°C time: 30 s/mm of thickness
Recommended austenitizing temperature: 1190 – 1220°C. The holding time should not be too long to avoid a risk of grain coarsening and a loss of toughness. It is recommended to keep the part at the austenitizing temperature 30 minutes per inch of thickness as soon as the temperature of the surface reach the austenitization temperature.
Quenching medium
Oil at 80°C, vacuum (pressure > 6 bars), salt bath 500 – 550°C.
To ensure good toughness, treatment with oil or salt bath is preferable.
After quenching the hardness is 64 – 67.5 HRC
Sub zero treatment
For parts that need to have high dimensional stability and to increase wear resistance without reducing toughness, it is recommended to perform a subzero treatment at a temperature between -70°C and -190°C for 1 hour for 25 mm of thickness of the part.
The temperature range from -70°C up to -120°C (named cold treatment of steel) leads to the complete transformation of austenite into martensite and as a consequence to better stability associated with improved hardness and better wear resistance. On the 3243 H PRIME such a treatment leads to an increase of 100% of the wear resistance (wear ratio). The temperature range from -135°C down to -190°C (named cryotreatment of steel) leads also to the complete transformation of austenite and also the precipitation of ultrafine carbides improving a lot the wear resistance without modification of the toughness and on 3243 H PRIME such a treatment leads to an increase of 200% of the wear resistance (wear ratio). This treatment is optional for common applications.
Tempering
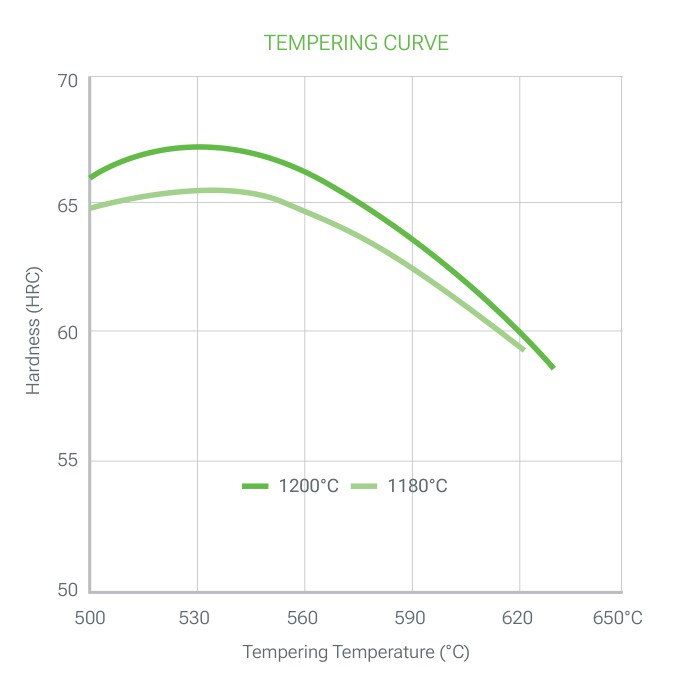
To ensure a minimum residual austenite rate as well as greater tool stability, it is essential to perform a double (triple is better) tempering. Each tempering is followed by a cooling under 100°C.
Each tempering time must be at least equal to 1h + 1h for 25 mm of thickness of the treated part (equivalent thermal thickness).
Surface treatment
PVD, CVD
3243 H PRIME is suitable for all kinds of PVD and CVD treatment as soon as the treatment temperature is 30°C lower than the last tempering temperature.
Polishing
3243 H PRIME could be polished the treated state and can be used for applications requiring a sufficiently polish level for translucent parts. Optimal polishing is achieved by performing consecutive steps of fairly close roughness and stopping each step as soon as the last scratch of the previous step disappears.
Machining
The machining parameters below are given for information only and must be adapted according to the equipment and usual machining conditions.
Grinding in annealed conditions
| Carbide insert | Solid tool | ||
|---|---|---|---|
| Rough machining | ½ Finishing | Finishing | |
| Cutting speed m/min | 50 – 70 | 80 – 105 | 40 – 45 |
| Feed mm/r | 0.35 | 0.15 | 0.01 – 0.1 |
| Depth of cut mm | 2 – 3 | 1 – 1.5 | 0.01 – 0.1 |
Turning in annealed conditions
| Carbide insert | HSS tool | ||
|---|---|---|---|
| Rough turning | Finishing | Turning | |
| Cutting speed m/min | 90 – 110 | 115 – 130 | 15 |
| Feed mm/r | 0.35 | 0.15 | 0.1 – 0.2 |
| Depth of cut mm | 2 – 3 | 1 – 1.5 | 0.5 – 2.0 |
Drilling in annealed conditions
Carbide drill
| Insert | Solid | |
|---|---|---|
| Cutting speed m/min | 120 | 60 |
| Feed mm/r | 0.10 | 0.20 |
HSS twist drill
| Drill diameter mm | Cutting speed m/min | Feed mm/r |
|---|---|---|
| < 5 | 9 | 0.10 |
| 5 – 10 | 0.17 | |
| 10 – 15 | 0.22 | |
| 15 – 20 | 0.30 |
Fine grinding
General indications for grinding wheels to be used on 3243 H PRIME in the heat treated condition
Usually, rather soft vitrified aluminum oxide grinding wheels (grades G for plane grinding to K for cylindrical grinding) are used.
Particular attention will be paid to effective cooling of the surface during grinding to prevent degradation of the material surface.
Electro-discharge machining
3243 H PRIME is also suitable for EDM machining (wire or electrode). Preferably, the machining will be carried out with a low current density and a high frequency in order to limit the thickness of the white layer as much as possible.
Then it is necessary to carry out a stress relieving at 25°C below the last tempering in order to reduce the level of residual stresses (which could lead to a risk of cracking) and to carry out a polishing to completely remove the white layer formed during the discharge machining process.
Welding
3247 PRIME cannot be welded.
Download the 3243 H PRIME datasheet (PDF)
More grades: High Speed Steels. Where to buy: Service Network.
